
‹
›
‹
›
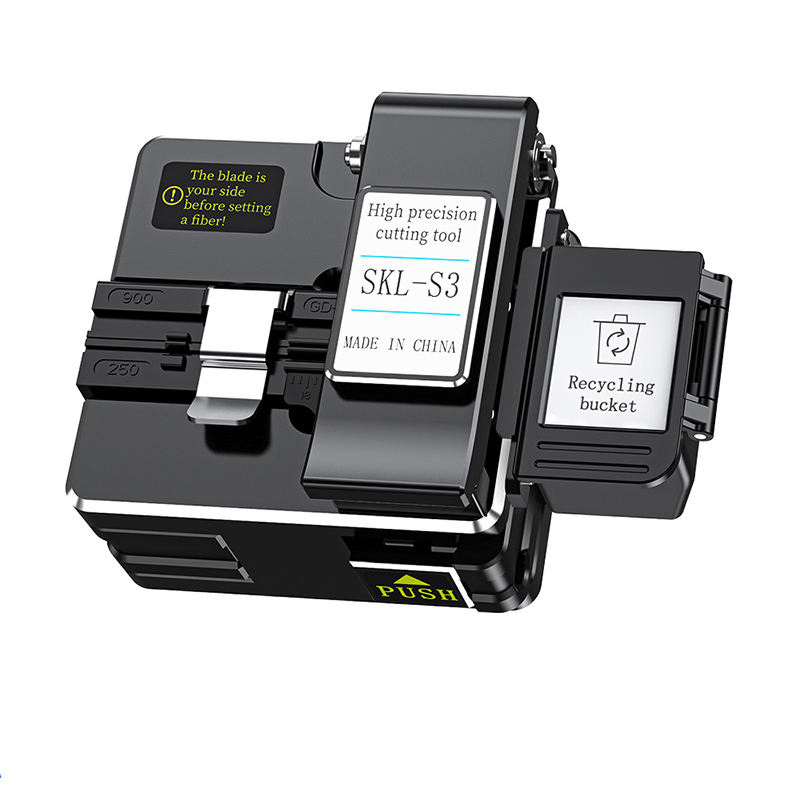
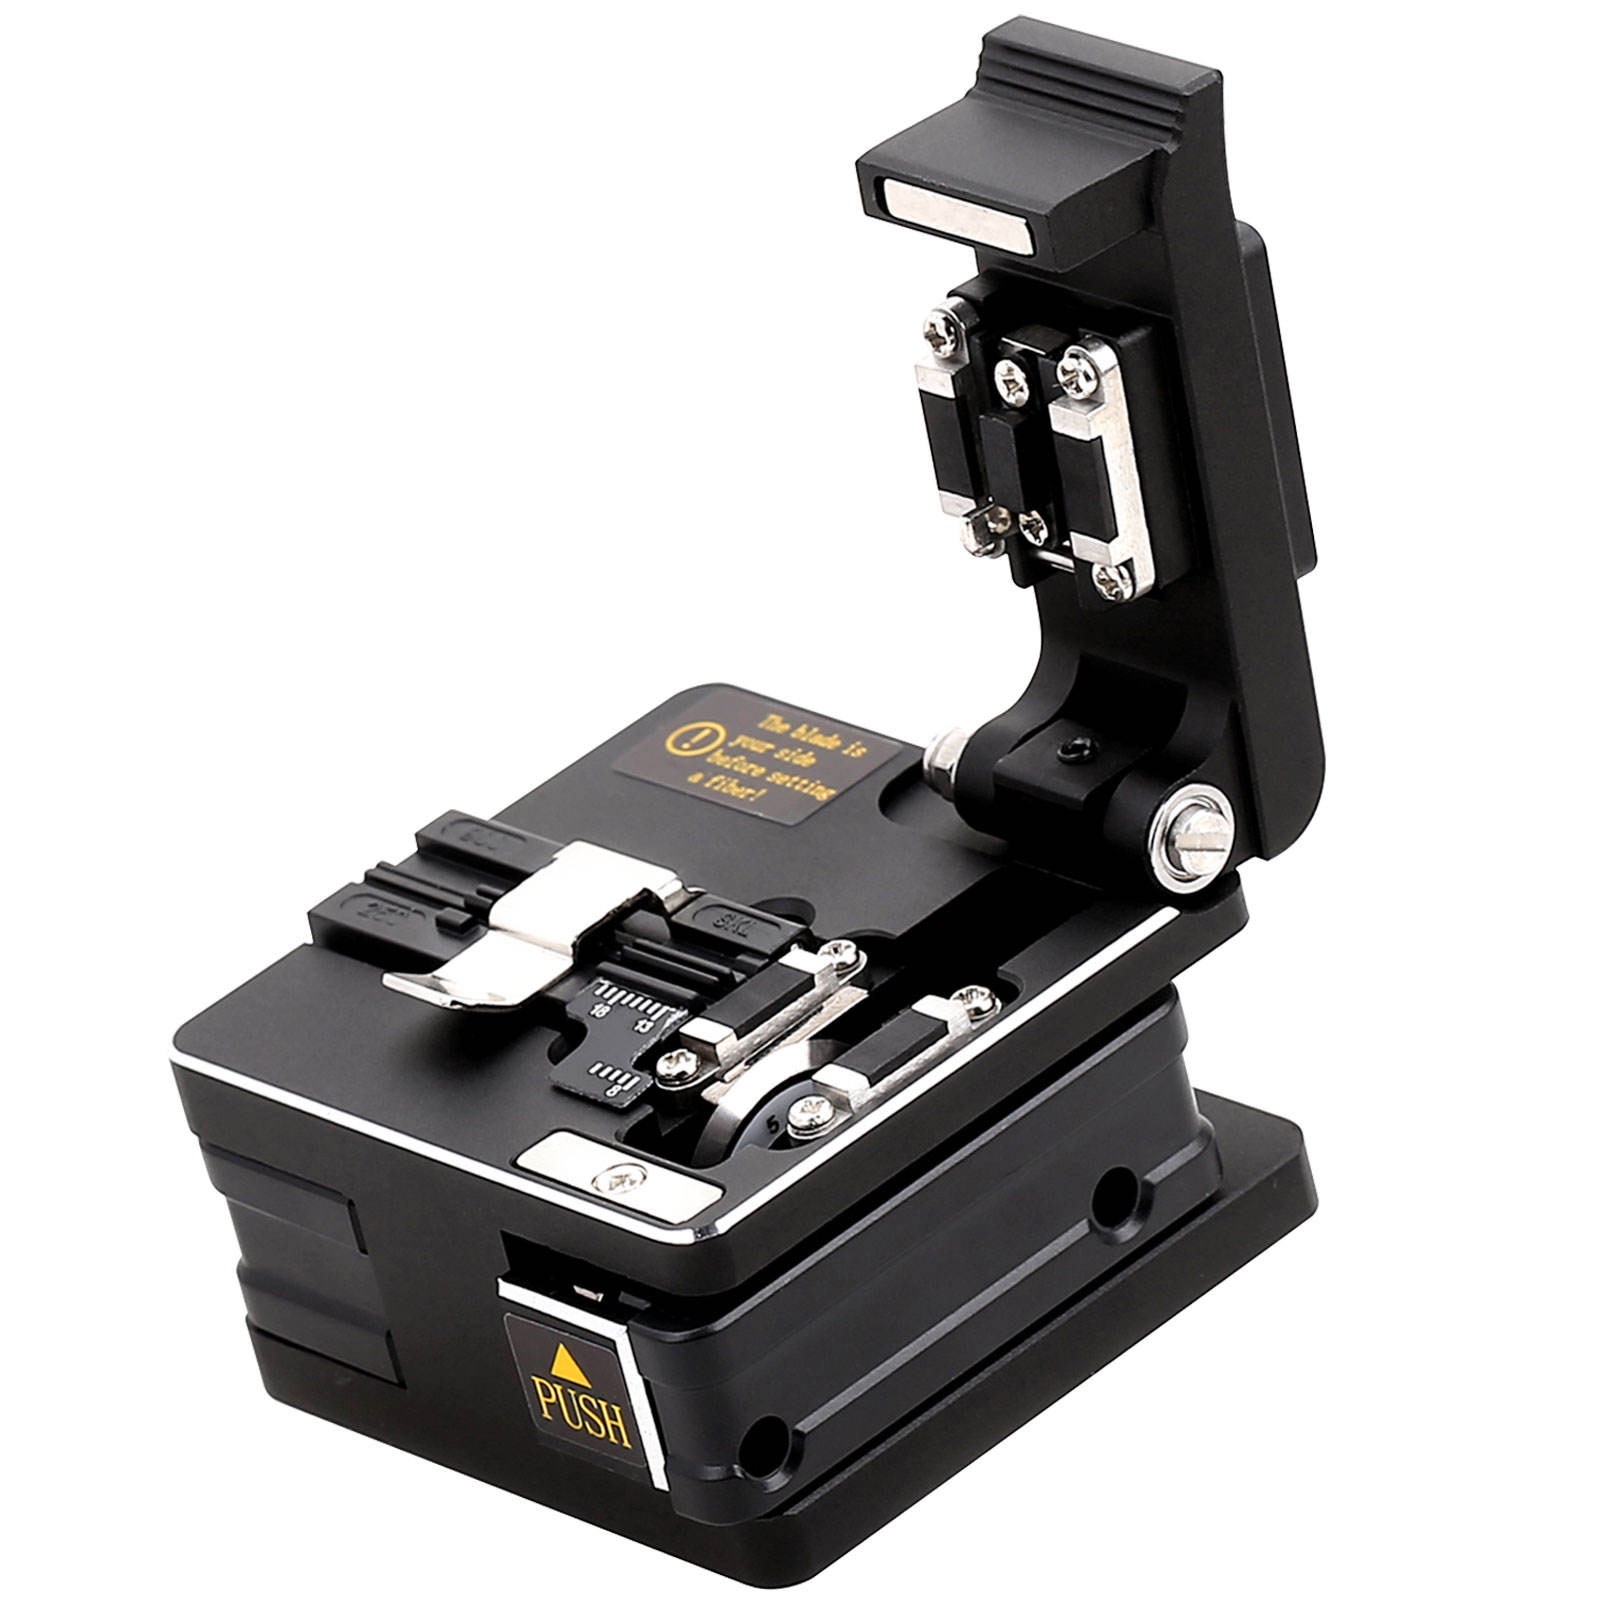
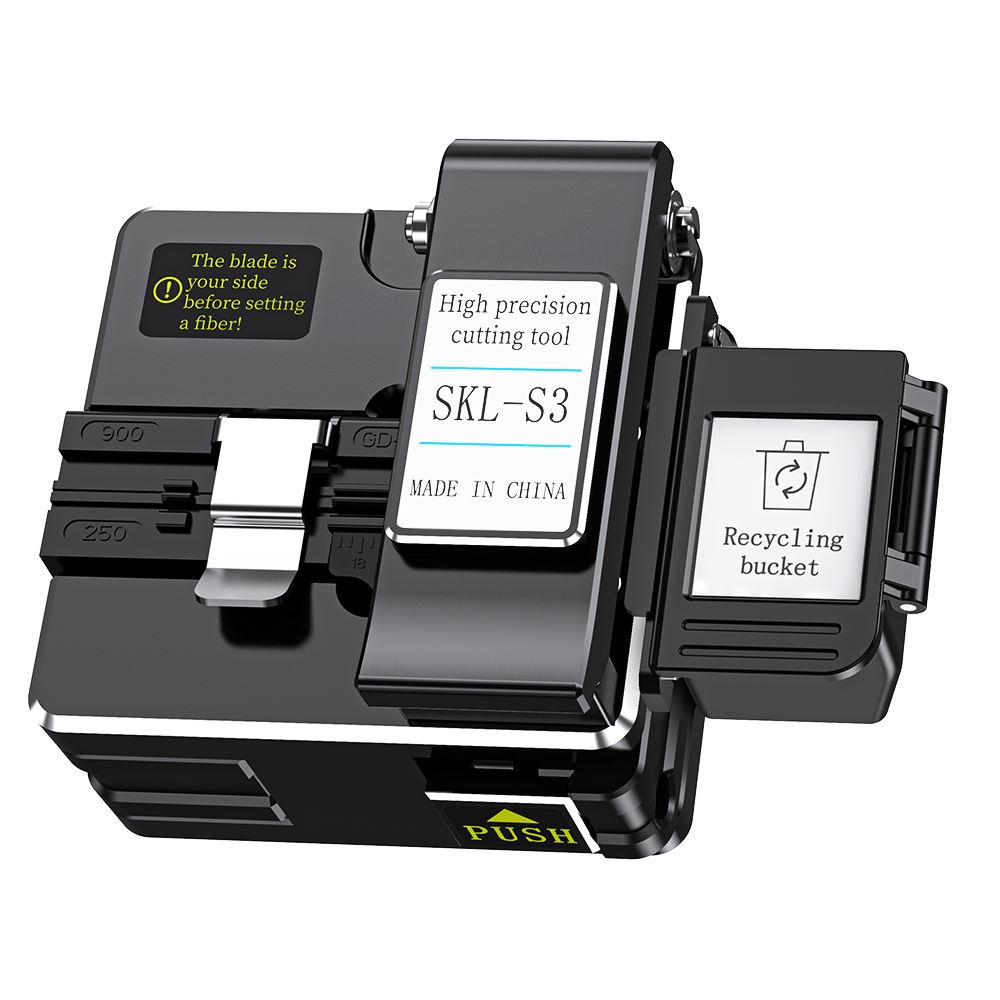
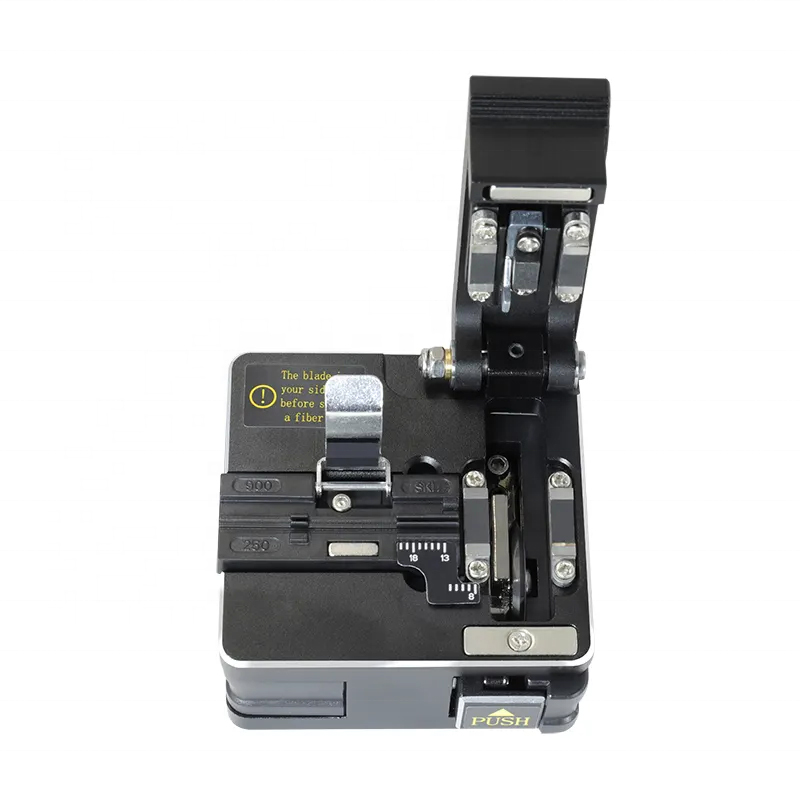
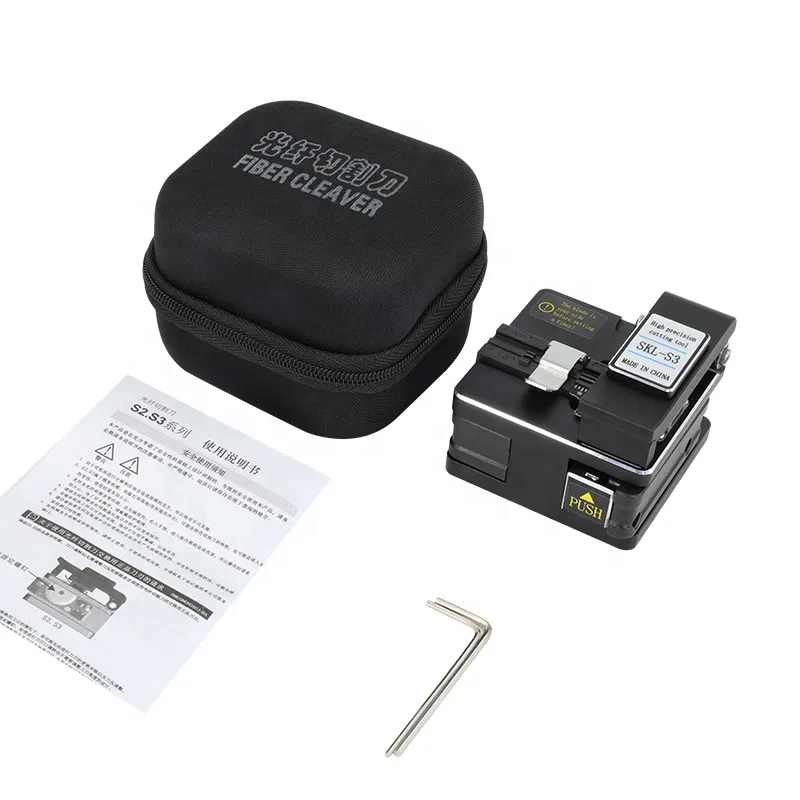
LF048 Wholesale SKLS3 Fiber Optic Cable Cleaver Durable Blade FTTH Network Construction Tools
Share on
SKLS3 Fiber Cleaver for Repeatable FTTH Fusion-Splice Preparation
SKLS3 fiber cleaver is a mechanical preparation tool for producing a flat, repeatable end face on stripped optical fibre before fusion splicing, mechanical splicing or connector termination. Its commercial value is not the number of cuts printed on the box; it is the ability to deliver stable cleave geometry across technicians, blade positions and field conditions.
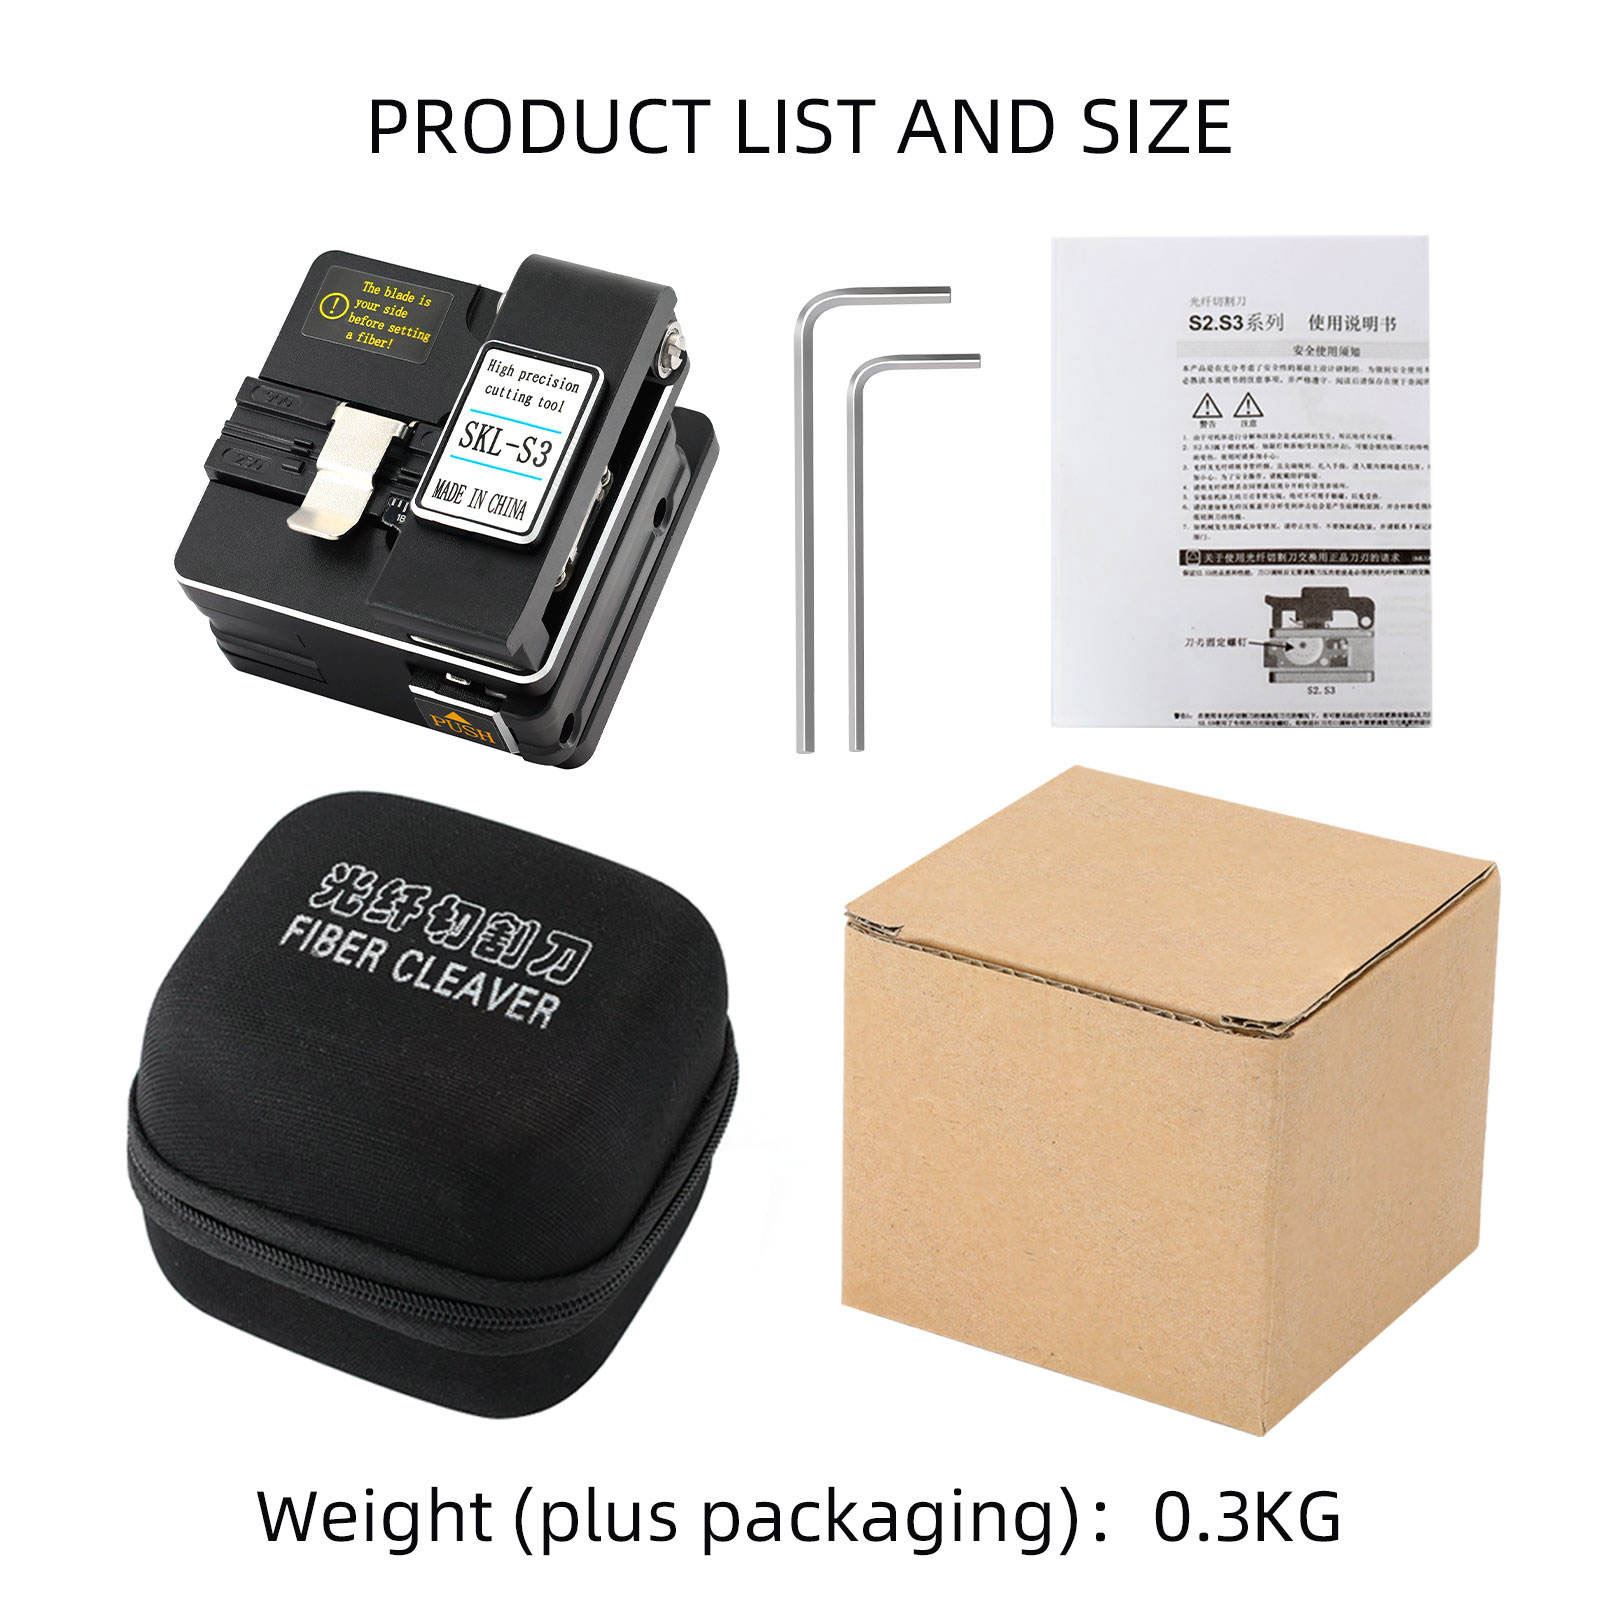
SKLS3 uses one-step press action with automatic blade return and is best suited to high-volume FTTH drop-cable and pigtail preparation where technicians want a compact universal fixture and repeatable operating sequence. LinkFiber can supply the cleaver as a stand-alone tool or as part of a project kit with the matched stripper, cleaning materials, spare blade, carrying case and work instruction.
Best Fit in a Fiber Splicing Workflow
A fibre cleaver never cuts an intact 2.0 × 3.0 mm drop cable or a jacketed jumper directly. A multi-slot fixture may hold the prepared cable or coated fibre, but the cable jacket, strength members and coating must first be stripped so the blade contacts clean 125 µm glass. This distinction prevents broken blades, poor end faces and unsafe glass fragments.
Model Selection and Configuration Control
Choose SKLS3 when a standardized one-step workflow and fixed prepared-fibre length suit the splice protector, fast connector or splicer holder used by the project.
The existing specification lists a fixed 18 mm prepared-fibre length, 16 indexed blade positions and a supplier-stated total design life of at least 48,000 cleaves. These are purchase specifications to verify on the approved sample; actual blade life depends on glass cleanliness, blade height, indexed position and maintenance.
Before purchasing, confirm coating diameter, cladding diameter, prepared-fibre length, holder type, single or ribbon construction, blade code, spare-blade availability, waste-collection method and the operator sequence. Photographs alone are insufficient because similar housings may contain different holders or adjustment systems.
Technical Specifications
What the Cleaver Actually Controls
The cleaver creates a controlled fracture in the glass. It does not polish the end face and it cannot by itself guarantee splice loss. The result depends on the blade edge initiating the crack, correct bending stress, stable clamping and a fibre free from coating residue. Fusion-splicer cleave-angle estimates are useful process indicators, but they are not a substitute for inspecting a representative sample and monitoring actual splice performance.
Single-mode and multimode fibres normally share a 125 µm cladding diameter, but coating, bend sensitivity, ribbon geometry and holder requirements vary. G.652.D and G.657.A access fibres can be processed when the holder and stripped length are correct; unusual coatings, fibres above standard cladding diameter or specialty fibres require project testing.
Blade Life, Position Indexing and Adjustment
Published blade life is normally a design estimate derived from multiple indexed edge positions. It should not be treated as a guaranteed number of acceptable cleaves without maintenance. A blade position should be advanced only after cleaning, fibre preparation and loading have been ruled out. Blade height changes fracture geometry and should be adjusted with the supplied tool in small controlled steps, then validated with a cleave sample—not changed to chase one poor splice.
Common Cleaving Failures and Prevention
Pre-shipment Quality and Acceptance Plan
For a B2B order, LinkFiber can qualify the exact cleaver, blade and holder combination against a written inspection plan. A practical lot check uses the buyer’s representative fibre and stripper, performs repeated cleaves across selected units, reviews the end-face image or splicer cleave-angle estimate and records defects, operating feel, scrap collection and accessory completeness.
- Approve one exact model and blade/holder construction before volume production.
- Test a representative sequence rather than reporting only one best cleave.
- Record fibre type, coating diameter, prepared length, blade position and operator.
- Set acceptance limits for angle distribution, visible defects and successful splice rate.
- Verify blade indexing, adjustment tool, waste box or scrap-control method and spare-part supply.
- Check protective packing, label, manual and ordered accessories before shipment.
B2B Buyer Guide: Information Required for an Accurate Quote
Send the fibre or cable type, cladding and coating diameter, single or ribbon count, target prepared-fibre length, fusion-splicer or fast-connector model, expected daily workload, quantity, destination, spare-blade requirement and private-label needs. For tenders, add the inspection method, sampling level, required reports and exact compliance documents.
For medium-sized contractors and distributors, total cost should include blade availability, repeatability, technician training time, fixture compatibility, scrap safety and after-sales adjustment support. A cheaper cleaver that causes repeat splices, wasted sleeves and return visits can cost more than the tool itself.
MOQ, Samples, Lead Time and Packing
Related Fiber Installation Tools
Compare other models in the Fiber Cleaver range or build a complete field kit from Fiber Optic Installation Tools. Related choices include the SKLS3 cleaver, Signal Fire S09, SKL6C and FC6S. LinkFiber can match the cleaver with strippers, cleaning tools, spare blades and fusion-splicing equipment under one approved packing list.
Why does the SKLS3 achieve a blade life of 48,000 cuts? How is it different from ordinary cleavers?
What is the cutting angle performance of this SKLS3 cleaver? Can it meet the requirements of high-performance fusion splicers?
Can the SKLS3 cleave a 2.5mm jumper cable directly?
To learn more about this product, you can submit your requirements here.
 LF102 Signal Fire AI-12 6-Motor Core Alignment Fusion Splicer
 LF036 Metal Hard Case FTTH Fiber Optic Installation Tool Set
 Signal Fire AI9 Fiber Optic Fusion Splicer with VFL OPM
 LF046 6 Motors Core Alignment Fiber Optic Fusion Splicer 0.01dB Low Loss Trunk Line Telecom Equipment
 LF-054-Adjustable Longitudinal Fiber Cable Stripper Round Optical Fiber Jacket Slitting Cutter
 Signal Fire AI6A+ Fusion Splicer 6 Motors Core Alignment with OPM
 Signal Fire AI7C Fusion Splicer Wholesale Price
 LF041 Signal Fire AI30 Fiber Optic Splicing Machine Full Set Fusion Splicer with Tool Kits
 LF043 High Quality China Made Optical Fiber Fusion Splicer Telecom Equipment Low Loss
 LF048 Wholesale SKLS3 Fiber Optic Cable Cleaver Durable Blade FTTH Network Construction Tools
 LF050 Q1S Automatic Fiber Optic Cleaver
 LF051 S09 Telecom Grade Low Cut Angle Fiber Optic Cleaver Precise Optical Fiber Splicing Cutting Tool
Professional Consultation
If you are interested in our products and would like to know more details, please leave a message here, and we will get back to you as soon as possible.


